Boron Carbide Company: Key Factors for Selecting a Reliable Advanced Ceramics Partner
2026-09-20
What truly sets a reliable boron carbide company apart? It’s rarely the spec sheet alone—it’s the supplier’s ability to replicate results batch after batch and adapt when your process hits a snag. After years in the field, HUAYI TECH has learned that choosing a partner is less about a single transaction and more about engineering alignment. Here are the key factors we recommend weighing before you sign off.
Check Purity Claims Against Independent Test Results
When a supplement label boasts 99% purity, that number means little until it's held against data from an unaffiliated lab. Pull the certificate of analysis from the manufacturer's site, then look for a batch number that matches the bottle in your hand. If the COA is missing, outdated, or vague about testing methods—like skipping heavy metal or residual solvent panels—treat the purity claim as marketing rather than fact.
Independent verification goes deeper than a single number. Compare the lab's quantification of the active compound against what's printed on the label, and note whether the testing facility follows recognized protocols such as USP or ISO standards. A third-party result that shows 97% purity when the label claims 99% isn't necessarily a dealbreaker, but repeated discrepancies across batches suggest the company isn't controlling its supply chain.
Don't settle for a PDF that could be photoshopped. Many reputable certifiers—NSF, USP, or Eurofins—let you enter a lot code on their website to view the original report. If the brand refuses to name its testing partner or hides the full report behind a 'proprietary' excuse, that opacity is a stronger signal than any purity percentage printed on the front of the jar.
Look for Proven Experience With Ballistic-Grade Components
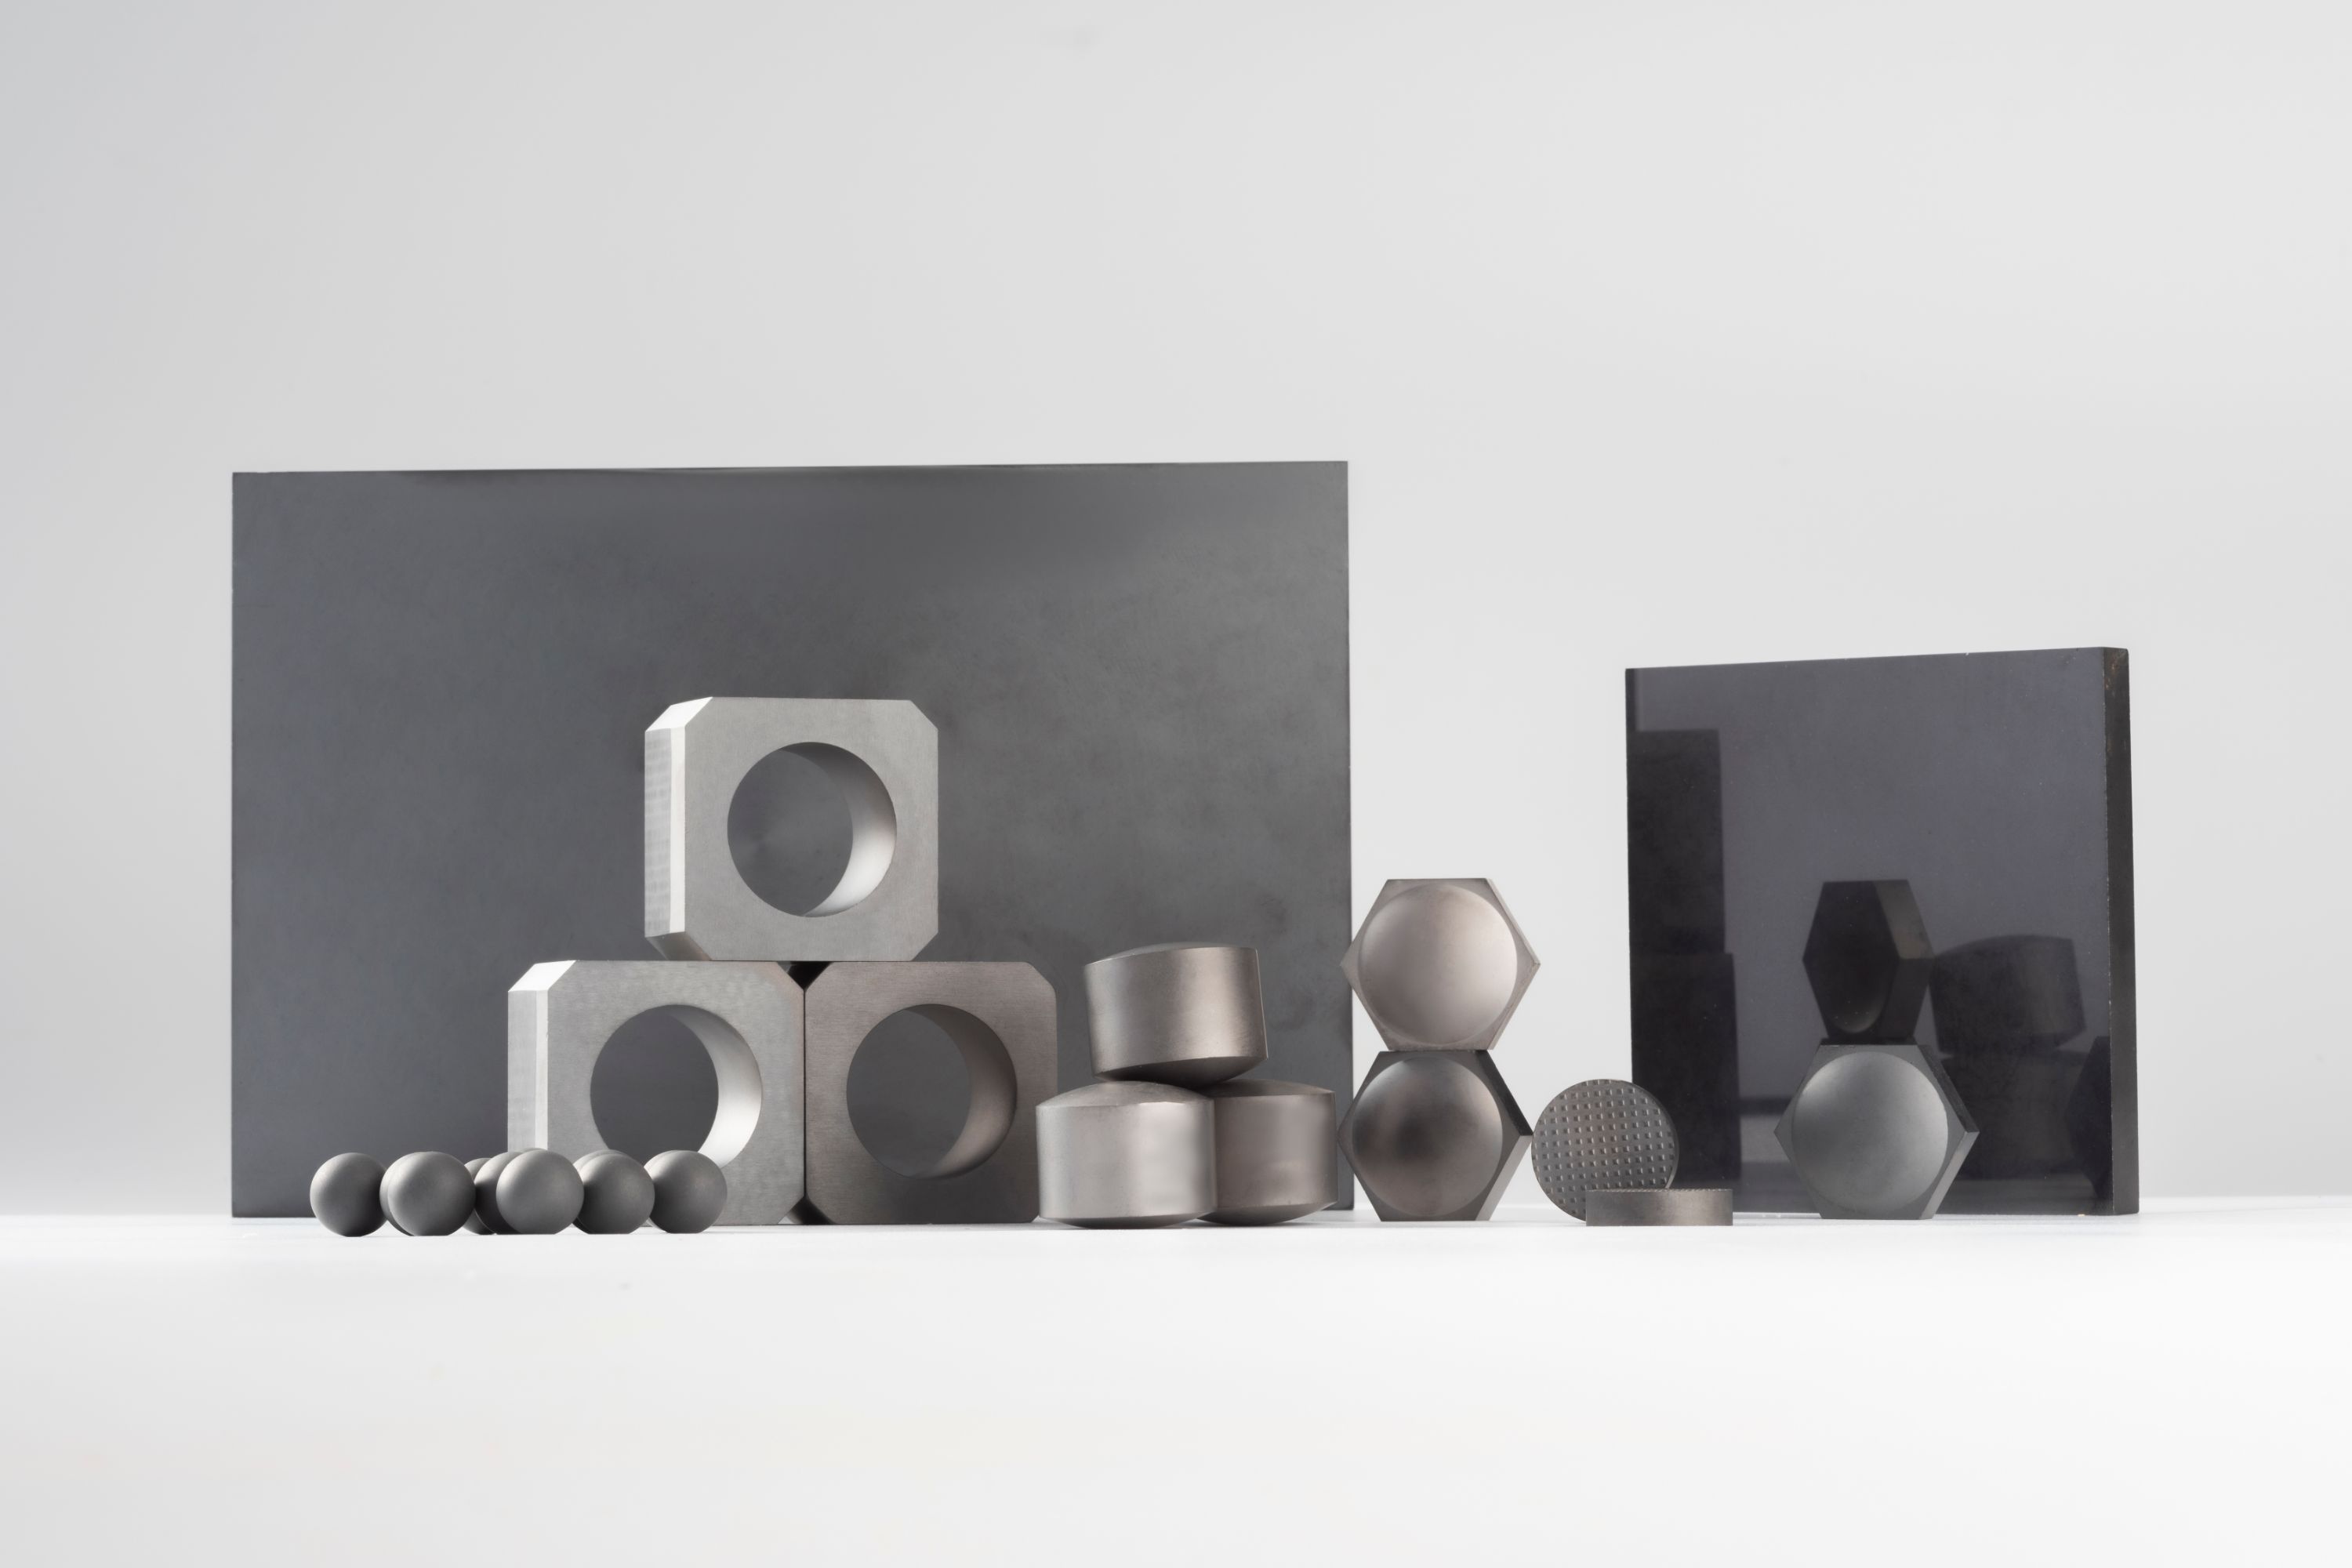
Ballistic-grade materials behave differently under stress than their commercial counterparts, and only a specialist who has spent years machining, welding, and testing them knows where the weak points hide. Ask directly about previous projects involving armor steel, ceramic strike faces, or ultra-high-molecular-weight polyethylene. The details matter: how they controlled heat input to avoid compromising the plate's integrity, which fasteners they selected to prevent galvanic corrosion, and what documentation they provided for traceability. A shop that can walk you through these specifics without hesitation has likely earned its stripes the hard way.
Don't settle for vague claims like "military-grade" or "combat proven." Push for concrete examples—perhaps a run of rifle-rated door panels for cash-in-transit vehicles, or a batch of spall liners for a law enforcement robot. Each of those jobs leaves a trail of lessons: tolerances that shifted after ceramic tile bonding, edge geometry that changed how a plate absorbed a second hit, or packaging that kept moisture out during six months of storage. A fabricator with real ballistic experience will volunteer these failures and fixes because they know that's where competence is built.
Finally, pay attention to how a supplier talks about testing. Those who have worked with ballistic-grade components understand that lab certificates are a starting point, not the whole story. They can explain why a certain batch of steel needed extra normalization before cutting, or why a particular adhesive system failed after temperature cycling. They won't promise miracles, but they will show you the test reports, the material certs, and—if you're lucky—a piece of scrap plate with a few dents from an actual live-fire session. That kind of hands-on evidence beats any marketing brochure.
Evaluate Quality Systems Beyond ISO Certification
A certification on the wall doesn’t tell you how a supplier actually handles nonconformities, how their operators react under pressure, or whether their internal audits uncover real problems instead of just checking boxes. Dig into the living parts of the quality system: review past corrective action reports, ask to see how they track and close issues, and look for evidence that lessons learned get fed back into training or process updates. A system that quietly improves month after month is worth more than a perfect paper trail.
Look for signals that quality thinking reaches the shop floor. Talk to line staff about what happens when they spot a defect—do they stop the line, tag the part, or just keep going? A strong system gives people the confidence to escalate problems without fear, and it shows up in simple tools like visual boards, last-minute change notes, and a maintenance log that actually gets filled in. If those things feel like theatre, the certification isn’t protecting your supply chain.
Finally, ask about how they handle borderline cases. Every factory faces parts that nearly pass, customers who waive specs, or rush orders that skip a step. What matters is whether they document those decisions, who signs off, and how they review them later. If a supplier can walk you through a recent bad call and what they changed afterward, you’re seeing a quality system that breathes. That’s the kind of partner you want on the other end of a purchase order.
Request Custom Material Trials Before Full Production
Most suppliers will tell you their standard materials are fine for your application, but that confidence rarely survives contact with your actual production line. Requesting a custom trial batch lets you test how the material behaves under your specific tooling, temperature swings, and handling methods—things a datasheet won't reveal.
When you put in the trial request, be specific about the parameters you need to validate: tolerance ranges, surface finish after secondary operations, and any subtle differences between the trial run and your normal throughput. A vague “just send us something to try” tends to produce a sample that passes in the lab but fails on your floor.
Treat the trial as a small insurance policy. The cost and lead time of a pre-production material run are minor compared to a recall, line stoppage, or rework caused by a material that only failed when scaled. It also gives the supplier a clear reason to pay attention to your account from the start.
Assess Supply Chain Redundancy and Inventory Buffers
Mapping redundancy starts with a clear-eyed look at every node and lane. It is not enough to know you have a backup supplier on paper; you need to test whether that alternate can actually ramp up when your primary line goes down. The same logic applies to internal throughput—equipment, shifts, and even software systems that quietly share a single point of failure.
Inventory buffers often get treated as a cost to be minimized, but that misses their role as shock absorbers. The question is not whether to hold buffer stock, but where and how much. Segment your SKUs by volatility and lead-time risk. Items with erratic demand or long, concentrated supply chains usually justify deeper buffers, while stable, locally sourced goods can run lean without hurting service levels.
Then bring these two views together. Cross-check each critical path: if a port closes for a week, does your buffer cover the gap until the alternate routing is live? If a key component's lead time doubles, does your safety stock calculation still hold? Frequent, scenario-based reviews—not annual spreadsheet updates—keep redundancy and inventory aligned with real exposure.
Prioritize Long-Term Technical Collaboration Over One-Off Sales
Short-term wins from a single transaction rarely reflect the depth of value that emerges when engineering teams work side by side over months or years. A project sold as a one-off might solve an immediate pain point, but it leaves the harder, more interesting problems untouched. Long-term technical collaboration shifts the focus from delivering a fixed scope to building shared understanding: your team learns how our systems behave under real conditions, and we adapt our approach to the quirks of your infrastructure. That kind of mutual calibration doesn't happen in a single sprint.
When we treat a sale as the start of a relationship rather than the finish line, the incentives line up differently. Instead of polishing a demo for a procurement committee, we spend time diagnosing failures that only appear after launch. Instead of guarding our code behind restrictive licenses, we open up the parts that help your internal team extend and maintain the solution. The result is less rework, fewer surprise costs, and a technical foundation that can evolve as your product roadmap shifts.
Of course, not every engagement needs to become a multi-year partnership. But for anything involving complex integration, performance tuning, or ongoing security updates, a transactional mindset often costs more in the long run. We'd rather invest early in understanding your stack, your release cadence, and your team's constraints than bill for a quick fix that falls apart after the next major version bump. That's what prioritizing long-term technical collaboration actually looks like in practice.
FAQ
It sits just below diamond and cubic boron nitride in hardness, yet its density is much lower than most engineering ceramics. That means you get outstanding erosion resistance without adding excessive weight—critical in body armor, helicopter seats, and sandblasting nozzles.
Ask for destructive test data from each production lot, including density, hardness, flexural strength, and fracture toughness. A serious supplier won't just send a certificate of conformance; they'll share actual micrographs and show how they track sintering curves.
The starting powder dictates grain size distribution, oxygen content, and sintering activity. If the powder has broad particle size ranges or metal contamination, you'll end up with porous, weak spots that fail unpredictably under stress or thermal shock.
Density below 96% of theoretical usually means open porosity, which tanks strength and lets fluids or gases penetrate. A reliable partner will target at least 98% and demonstrate it with Archimedes or gas pycnometry measurements rather than just quoting a catalog number.
They should review your drawings, point out features that are hard to machine or prone to chipping, propose green machining allowances, and even suggest alternative grades if your environment has unexpected chemical exposure. That back-and-forth saves far more than a price discount.
Hot pressing and spark plasma sintering usually give finer grains and higher density than pressureless sintering, but they limit shape complexity. A capable partner understands the trade-offs and picks the method based on your geometry, tolerances, and budget instead of forcing one process on everything.
Yes. Look for ITAR registration, AS9100 certification, and Nadcap accreditation for special processes if parts go into aerospace or defense. For nuclear shielding, ask about traceability of raw powder lots and compliance with relevant radiation safety testing protocols.
They avoid sharing process details, deliver inconsistent density values between batches, don't have in-house SEM or mechanical testing, or can't provide references for similar applications. Reluctance to discuss failure modes is a major red flag because every ceramic design has limits.
Conclusion
Selecting a boron carbide partner starts with verifying what's actually in the material, not just what the data sheet claims. Reputable suppliers will happily share independent lab results for purity, grain size, and density—especially if you're sourcing ballistic-grade plates or tiles where a few percent of free carbon changes fracture behavior. Ask for past projects involving armor ceramics, nuclear shielding, or wear-resistant nozzles; real production history beats marketing brochures. Quality systems matter, but ISO 9001 alone tells you little about process control. Dig into how they handle incoming powder, sintering temperature drift, and final non-destructive testing. A supplier that can walk you through their scrap rate and corrective action log is far more valuable than one with a wall of certificates.
Before committing to full production, request custom material trials using your own pressing or machining parameters. This reveals not just whether the boron carbide meets spec, but whether the vendor communicates well under tight deadlines. Supply chain redundancy is another quiet killer—ask where their raw powder comes from and how much buffer stock they keep. If their only boron carbide source is a single overseas mill, your lead times are one geopolitical hiccup away from collapsing. Finally, prioritize partners who talk about long-term engineering collaboration: tweaking binder systems, adjusting sintering cycles for your geometry, or co-developing a next-generation composite. A one-off sale is easy; a partner who remembers your part number and calls when their process drifts is genuinely rare.
Contact Us
Contact Person: Junting Leo
Email: [email protected]
Tel/WhatsApp: +86 18615009766
Website: https://www.huayimaterial-china.com/