China Stainless Steel Cup Factory: Key Factors to Evaluate Before Placing Your First Order
2026-10-03
Most first orders from a China stainless steel cup factory fail long before production starts. The gap is rarely in the cups themselves—it’s in skipping the right evaluation steps: verifying raw materials, checking vacuum insulation samples, and pressure-testing the supplier’s lead times. If you’re preparing your first order, this post will show you exactly which factors to scrutinize. APEXAL brings factory-floor perspective to help you avoid the hidden traps that cheap quotes often disguise.
Reading the Steel: Verifying True Food-Grade Materials
When a supplier claims their steel is food-grade, the first place to look is the mill stamp. True 304 or 316 stainless carries a visible code—often “SUS304” or “AISI 316”—etched near the edge or on the underside. If that stamp is missing, faint, or deliberately buffed out, treat it as a red flag. Genuine food-contact steel also has a brushed or matte finish with no mirror polish, because too-high reflectivity can hide pitting or uneven alloy distribution.
Run your finger along the weld seams. On genuine food-grade material, the welds feel smooth and consistent, not rough or cratered. A rough weld indicates either a cheaper filler rod or overheating during fabrication, both of which can lead to micro-cracks where bacteria hide. Also check for any blue or rainbow tint near the seams—that is oxidation from excessive heat, and while it can be passivated, heavy discoloration often means the protective chromium layer was burned off.
Finally, ask for a material test report or at least a spark test if you are inspecting in person. Real 316 stainless throws short, reddish sparks with few forks, while lower-grade or coated steel throws longer, whiter sparks. If the seller hesitates to provide traceability or tries to tell you that all stainless is the same, walk away. Verifying food-grade steel is not about trusting a label—it is about reading the metal itself.
Capacity Reality Check: Will the Factory Meet Your Deadlines?
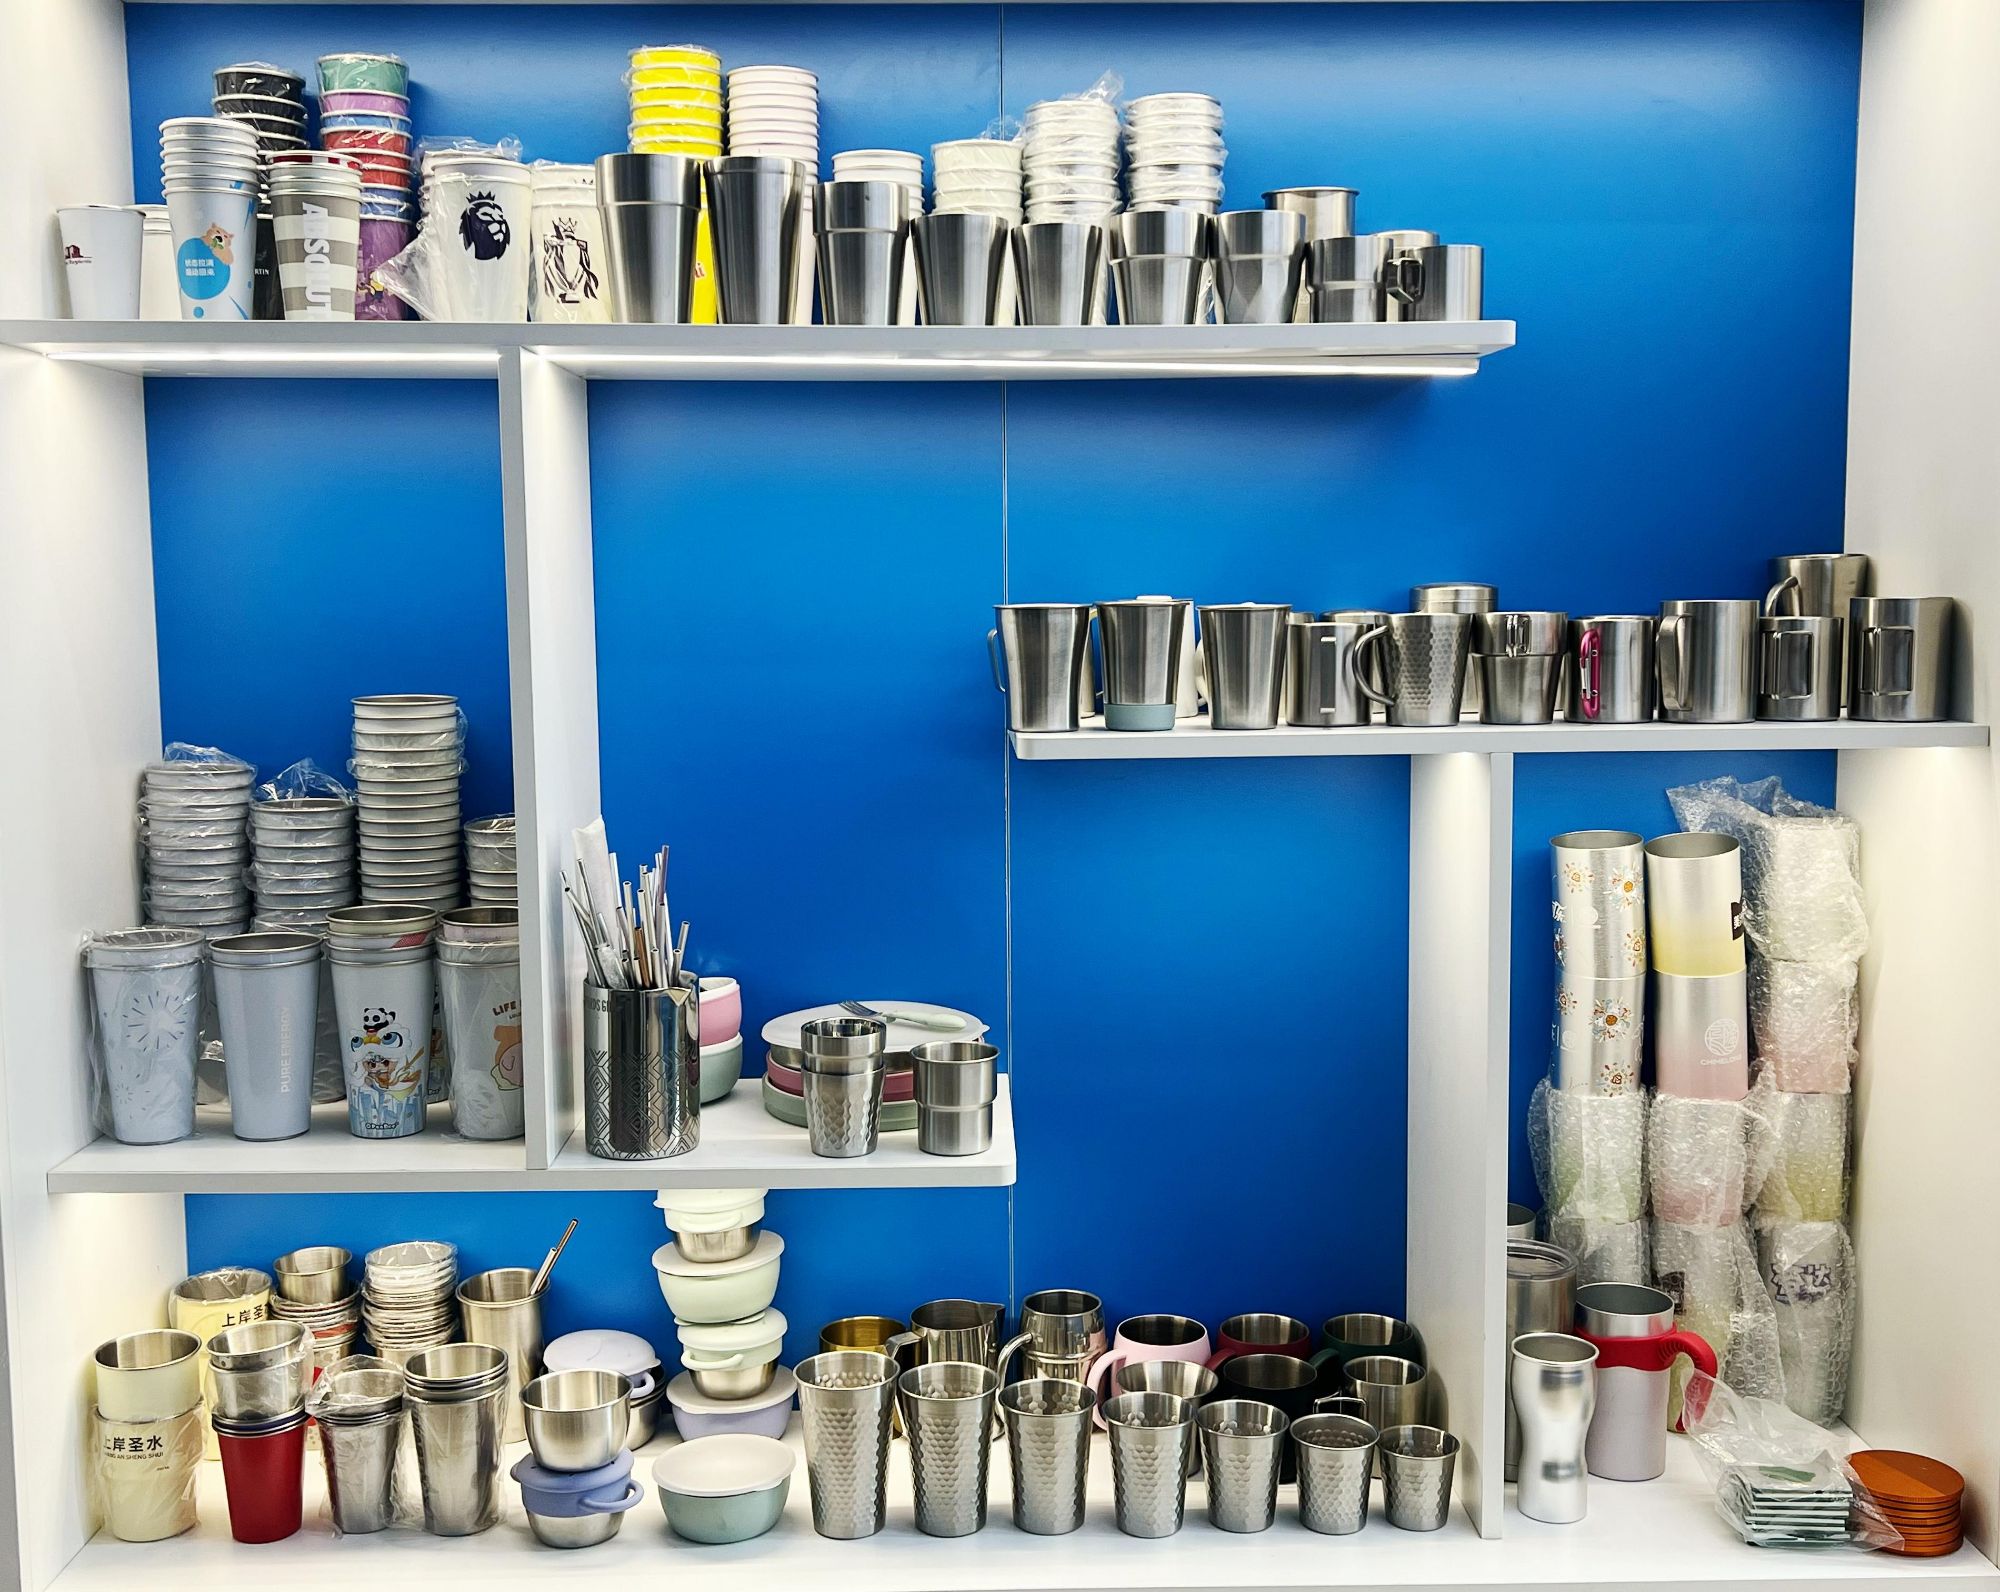
Many buyers only ask how many units the factory can produce per month, but that number is usually based on ideal conditions. What you actually need is the realistic output under your specific order mix, including changeover time, rework from quality checks, and material arrival delays. Ask for daily production records for similar items over the past six months, and if possible, stand on the floor and count finished cartons yourself instead of trusting a slide deck.
Bottlenecks are rarely about the total number of machines. More often, one specific process or skill set limits the whole line. For example, a product might need three experienced stitchers for a complex seam, and if one is absent or quits, the line stalls. Confirm whether the critical operations have enough cross-trained workers or backup capacity, and watch how long a changeover really takes when they switch from your product to someone else's.
Be alert to the optimistic lead time trap. A salesperson may promise 30 days while the actual production schedule needs 45, because they assume every raw material arrives on time, no machine breaks down, and no workers take leave. Ask the factory to show you the live production plan and what buffer they have if a key supplier is delayed by a week. Real capacity is not the best-case scenario; it is what happens on a normal Tuesday.
Custom Work Without the Guesswork: Design and Tooling Support
Every project starts with a clear picture, but turning that picture into a precise, repeatable process is where most operations stall. Our team works directly from your specifications, drawings, or even rough sketches to develop a build plan that removes ambiguity from the first cut to the final finish. This means no back-and-forth about tolerances, no assumptions about material behavior, and no last-minute tooling surprises that slow down delivery. Instead, you get a workflow that reflects how your parts actually need to be made.
Tooling is not treated as an afterthought. We design and build or source the fixtures, jigs, and custom attachments required for your specific geometry and volume. For short runs, we may use modular setups to keep costs down. For high-volume production, we invest in dedicated tooling that holds tighter tolerances and reduces cycle times. The result is a stable process that produces the same part on Monday as it does on Friday, regardless of who is running the machine.
If something in the design does not translate well to manufacturing, we flag it early and propose practical alternatives that preserve function while simplifying production. This collaborative step prevents costly rework and keeps your timeline intact. You do not need to be a machining expert to get expert results; you just need a partner who treats the details as seriously as you do.
The Quality Gauntlet: Inspections That Catch Problems Early
Most manufacturing defects don't announce themselves at the end of the line—they hide in a supplier's batch, a slight tool drift, or a rushed setup. The quality gauntlet is a deliberate series of early checkpoints placed before problems can compound. Instead of one final audit, this approach inserts short, focused inspections at raw material receiving, first-article approval, and in-process milestones. A warped bracket caught before welding costs minutes; the same bracket discovered after assembly costs a scrapped unit and a delayed order.
Each checkpoint uses the simplest tool that can do the job: a go/no-go gauge for a critical dimension, a visual standard for surface finish, or a quick torque test on fasteners. More advanced stations might employ coordinate measuring machines or automated optical comparators, but the goal isn't to inspect everything—it's to verify what changed since the last good part. When an inspection fails, the line pauses, root cause is traced, and the process gets corrected before the next cycle.
This gauntlet only works when inspectors and operators share the same mindset: catching a defect early is a win, not an interruption. Teams that log every nonconformance, no matter how small, build a history that points to recurring trouble spots—a dulling tool, a worn fixture, a supplier's inconsistent batch. Over time, early inspections become less about rejecting bad parts and more about tuning the process so fewer bad parts ever appear.
Communication Clarity: Early Signals of a Reliable Partner
Most people decide within the first few exchanges whether someone is worth trusting. One of the clearest early indicators is how plainly they speak. A reliable partner doesn't hide behind vague promises or wait for you to guess their intentions. They state what they can do, ask direct questions when something is unclear, and confirm details without being prompted. This isn't about being overly formal; it's about respecting your need to understand what's actually happening.
Pay attention to the small moments: when a deadline slips, do they tell you immediately with a reason and a revised plan, or do you hear about it only after chasing them? Clarity shows up in how they handle uncertainty too. Saying "I don't know yet, but I'll find out by tomorrow" is far more useful than a confident-sounding answer that later falls apart. These early patterns reveal whether the person sees communication as a two-way responsibility or just a way to manage impressions.
Over time, that early clarity becomes the backbone of reliability. Misunderstandings shrink, rework drops, and you spend less energy guessing. It's not the only trait that matters, but it's one you can spot almost immediately. If the first conversations leave you with more questions than answers, that's usually a sign the partnership will demand extra effort just to stay aligned.
The Real Cost Breakdown: Pricing, Payment Terms, and Hidden Fees
Most pricing pages only tell you the base rate. The actual number on your invoice depends on things like per-seat charges, storage overages, API call limits, and add-on modules that were never mentioned during the demo. A $49/month plan can easily become $160 once you activate two integrations, bump up your contact tier, and pay for priority support. Always ask for a full line-item breakdown before signing, not just the sticker price.
Payment terms are where a lot of the real cost hides. Annual billing might knock 20% off the monthly rate, but it also locks you in and often auto-renews unless you cancel within a narrow window. Monthly plans give flexibility but usually come with a higher effective rate and sometimes a setup fee that isn't refundable. Look for clauses about mid-contract price increases, change-of-terms fees, or penalties for reducing seats.
Hidden fees rarely appear on the pricing page. Common ones include data migration charges, onboarding or training costs, transaction fees per invoice, and extra fees for exceeding "fair use" limits. Before you commit, run a small pilot with real usage patterns and ask the vendor to confirm in writing exactly what is included at your chosen tier. That way, the first invoice won't be a surprise.
FAQ
Start by verifying how long the factory has actually been producing stainless steel drinkware and whether they have in-house tooling and polishing lines. Ask for real production videos, not just brochures, and confirm they can show recent export documents for your target market. This quickly filters out trading companies posing as manufacturers.
Request the mill certificate for the exact grade they plan to use—304 or 316 are common for cups. A reliable factory won't hesitate to share third-party lab test reports for heavy metals and overall migration. Also ask if they can run a salt spray test on the finished cup to catch rust issues before mass production.
Most dedicated cup factories in China set MOQ around 500 to 1,000 pieces for standard models, but this can rise quickly if you need custom molds or unique lid assemblies. Don't just accept the MOQ at face value—clarify whether it applies per color, per size, or per design. That distinction can make a huge difference in your landed cost.
Yes, but you need to nail down the mold ownership and per-cavity costs upfront. Some factories quote a low unit price then charge separately for the 3D drawing, mold opening, and sample revisions. Ask for a written breakdown showing which fees are refundable once production hits a certain volume.
Look for a dedicated QC team on site and ask how many inspection points they use per line. A strong factory will do incoming raw material checks, in-line leak tests, vacuum tests for double-wall cups, and final AQL sampling before packing. If they can't describe these steps clearly or show you a QC checklist, treat that as a warning sign.
For standard products with existing molds, expect 25 to 35 days after deposit and artwork approval. Custom molds can add three to five weeks before production even starts. Always build in buffer time for Chinese holidays, especially around Spring Festival, and confirm whether the factory will prioritize your order over larger clients.
It often predicts how the rest of the project will go. A reliable factory will ask about your target market, filling temperature, and lid usage before sending samples. If they just push a stock sample without questions, they may not be thinking about your actual end users. Pay attention to response time and whether sales staff understand technical details.
Watch out for factories that refuse video calls, can't provide recent customer references, or ask for 100% payment upfront. Also be wary if the price is significantly lower than three other quotes—that usually means thinner steel, cheaper plastic lids, or skipped polishing steps. A factory with nothing to hide will be transparent about their limitations.
Conclusion
Before committing to a stainless steel cup factory in China, you need to look beyond certificates and glossy sample photos. Ask for the mill test reports that trace the steel back to its heat number, and if possible, have a third party run a quick chemical analysis on a random cup from the production line. The difference between 304 and 201 stainless can be invisible to the eye but disastrous for food safety. At the same time, don't take stated monthly capacity at face value. Walk the floor during a live production run for a similar product, check how many lines are actually running, and ask what happens when a big order overlaps with your own. If the factory can't show you a realistic schedule with buffer days, your deadlines are already at risk. Custom work is another area where vague promises hide real costs: a factory with in-house tooling and an engineer who asks precise questions about wall thickness, lid tolerance, and vacuum insulation is far more likely to deliver a cup that works than one that just says "no problem" to everything.
Quality control should be a continuous loop, not a final checkbox. Look for factories that do inline inspections after each forming step, not just a final visual check before packing. Ask to see their rejection records and what triggers a line stoppage. If they hesitate to share that, treat it as a red flag. Communication in the early quoting stage tells you a lot: do they answer the question you actually asked, or do they reply with a template? Do they flag potential issues with your design before you place the order? That honesty is worth more than a lower unit price. Finally, get a full cost breakdown that includes tooling amortization, packaging, testing fees, and any loading or document charges. A factory that quotes only an ex-works unit price and then adds "unexpected" fees later will erode your margin quickly. Payment terms also matter—request a schedule tied to clear milestones, not a large upfront deposit, and confirm who pays for rework if the batch fails inspection.
Contact Us
Contact Person: Milo
Email: [email protected]
Tel/WhatsApp: +86 18621923991
Website: https://www.dgbaide.com