Professional Folding Carton Cutting Die Making Equipment – Key Considerations for Packaging Success
2026-09-04
Precision in folding carton cutting dies is rarely discussed until a job goes wrong — misaligned creases, crushed corners, or wasted board. Yet the equipment behind those dies decides your packaging’s final quality before a single box leaves the floor. This post unpacks the professional considerations that packaging buyers often overlook, from steel quality to repeatability, and why ADEWO is referenced by converters who treat every millimeter as a competitive edge.
Your Board Specs, Not the Tooling Catalog, Should Pick the Die Steel
The catalog lists a dozen grades with impressive hardness charts, but it knows nothing about your cycle times, your coolant setup, or the way your operator pushes the press a little harder on Friday afternoons. Starting with tooling catalogs flips the logic: you end up forcing your process into a steel choice instead of letting the process dictate what the steel must survive. Your board specs—hole sizes, edge radii, material thickness, bend angles, expected run volumes—are the real constraints. If you ignore them and pick a popular tool steel because it is on page three, you will pay for it in micro-chipping, premature wear, or unexpected breakage at the worst possible moment.
Think of the board as a fingerprint. A high-density board with tight pitch and small vias demands a die steel with fine grain structure and high compressive yield strength, not just high overall hardness. A thicker copper layer might call for better thermal conductivity to manage heat build-up during punching. The tooling catalog cannot see your board stack-up or your plating finish, but your specs do. Write down the worst-case scenario: maximum copper weight, minimum web thickness, hardest laminate filler, then let those numbers drive the steel grade. Only after that does the catalog become useful—as a shortlist of candidates, not a decision maker.
A common mistake is matching steel to the punch shape without considering the stripper plate and die clearance. Your board specs will tell you the required clearance as a percentage of material thickness; some steels tolerate tight clearances better than others because they resist edge rounding. Ask your steel supplier for a grade that holds its edge profile at your specific clearance, not one that simply scores high on a generic wear test. When the steel choice follows the board specs, you get fewer tool changes, less burr formation, and a die that outlasts three catalog-driven guesses.
Creasing Depth Is Where Cartons Earn Their Fold, or Lose Their Edge
Creasing depth is the quiet negotiator between board strength and foldability. Too deep, and you crush the fibers before the carton ever reaches a customer—corners look soft, sidewalls lose stiffness, and the structure feels tired. Too shallow, and the outer liner stretches past its limit, splintering along the hinge or springing back instead of holding a crisp right angle.
The ideal depth rarely matches the nominal caliper printed on a spec sheet. Recycled board folds differently after a humid night, and a worn die rule can drift half a millimeter across a long run without anyone noticing. That’s why checking the first few hundred cartons matters more than trusting a setup card.
A practical habit is to flex one scored sample back and forth, then slice through the crease with a blade. If you see compressed but intact fibers on the inside and a clean, unbroken outside surface, the depth is in the right neighborhood. Move the rule in tiny steps—sometimes a fifth of a millimeter separates a box that folds like it means it from one that cracks under pressure.
Stripping Pins Are the Unsung Heroes of Consistent Makeready
On any offset press, the difference between a clean run and a frustrating afternoon often comes down to details nobody notices until they bite back. Stripping pins are exactly that kind of detail. These small, precisely machined guides sit on the feed board or cylinder and keep each sheet moving through the press in perfect register. When they are set correctly, makeready feels almost boring—no skew, no misfeeds, no ghosted images drifting off the trim line. But the moment one pin is off by a fraction of a millimeter, you will chase the problem through blankets, packing, and plate bends before you finally look down and see the real culprit.
What makes stripping pins so easy to overlook is that they do not actively print anything. They never show up in a job jacket or a press check sheet. Yet their influence touches every single sheet in the run. A well-worn pin with a flat spot can cause intermittent side guide errors that drive operators crazy because they appear random. A pin set too high can snag lightweight stocks, while one set too low lets heavier boards wander. Consistency in makeready is not just about getting the first sheet right—it is about making the ten-thousandth sheet land exactly where the first one did. Stripping pins make that possible, provided someone remembers to inspect them with the same care given to rollers and dampening systems.
The best press operators treat stripping pins as a maintenance checkpoint, not an afterthought. A quick visual check for nicks, burrs, or uneven wear before the run starts saves hours of mid-job troubleshooting. Some old-timers keep a set of spare pins in their toolbox, not because they fail often, but because they know that a fresh, properly adjusted pin is the cheapest insurance against registration drift. In a world of digital controls and automated wash-ups, these mechanical heroes still earn their keep silently—one sheet at a time, run after run.
Faster Presses Expose Die Alignment Mistakes in the First Thousand Sheets
When a press runs at higher speeds, small misalignments in the die that would otherwise go unnoticed become impossible to ignore. The first thousand sheets act as an accelerated stress test—each cycle adds mechanical vibration and thermal expansion, causing even a fraction of a millimeter of drift to translate into visible register errors, uneven cuts, or ghosting.
Operators often mistake these early defects for material inconsistencies or operator error, but the root cause is usually alignment. A die that was perfectly set at slow speed can walk out of position once the ram cycles faster and the frame flexes under load. Checking pin locations, bolster flatness, and guide wear before a full production run can save hundreds of wasted sheets.
The quickest way to confirm a die alignment issue is to stop the press at sheet 200 or 300 and inspect a sample against the original setup sheet. If the deviation grows with speed, the alignment needs correction rather than compensation. Making small adjustments early prevents the first thousand sheets from becoming a pile of costly scrap.
A Daily Honing Habit Keeps Cutting Rules Sharp and Cartons Flowing
Sharp rules are the silent workhorses behind every carton that ships on time. When operators make a point of touching up the cutting edge each morning, they stop the kind of microscopic dulling that forces extra pressure, tears fiber, and leaves ragged scores. It rarely takes more than ten minutes, yet that small ritual prevents the cascade of adjustments that eat up an afternoon.
The habit pays off most visibly in the rhythm of the die-cutter. A rule that's honed daily glides through board without snatching or vibrating, so sheets move at the machine's intended speed instead of slowing down to nurse a struggling cut. That steadiness shows up in cleaner creases, fewer jam-ups at the stripping station, and pallets that stack flat without hand-finishing.
Shops that stick to this routine build a kind of mechanical memory. The rule's bevel stays true, wear spreads evenly, and the next full sharpening becomes a quick touch-up rather than a reconstruction. Cartons keep flowing not because anyone made a heroic fix, but because a small, boring, daily action kept the edge exactly where it belongs.
What the Tooling Quote Hides: True Cost per Million Finished Cartons
Most converters stop at the number on the tooling quote, but that figure rarely reflects what your cartons actually cost once the press starts running. A tool that's cheaper up front can chew through more board, demand more frequent stops, and leave you with finishing bottlenecks that inflate the real spend per million finished cartons. The gap between the quoted price and true production cost often hides in things like makeready waste, run speed ceilings, and the number of touchpoints required after die-cutting.
To see the true cost, you need to shift from asking "what does the tool cost?" to "what does it cost me to produce a million cartons with this tool in place?" That means factoring in board caliper consistency, the tool's tolerance stack, how quickly it wears, and whether it forces secondary operations that eat margin. A tool that runs at 5% lower speed or adds one extra strip-and-repack step can wipe out its initial savings within a single high-volume job.
Forward-thinking packaging operations are now pricing tools by their contribution to total carton economics, not by the invoice line alone. They request run-rate guarantees, ask for scrap-rate benchmarks at specific press speeds, and compare the cost of board lost during setup against the tool's lifespan. When you put all of that on one spreadsheet, the "cheap" tool often turns out to be the most expensive choice you can make.
FAQ
Professional systems are built around tight tolerances—often within ±0.05 mm—for consistent crease depths and knife positions across long runs. They also handle the specific rule heights and bevels used in folding cartons, which standard flatbed cutters might not accommodate reliably.
Thicker board requires more robust ejection and deeper crease channels. Machines with adjustable cutting pressure and programmable height settings let you switch between 200 gsm and 600 gsm stock without rebuilding dies or sacrificing edge quality.
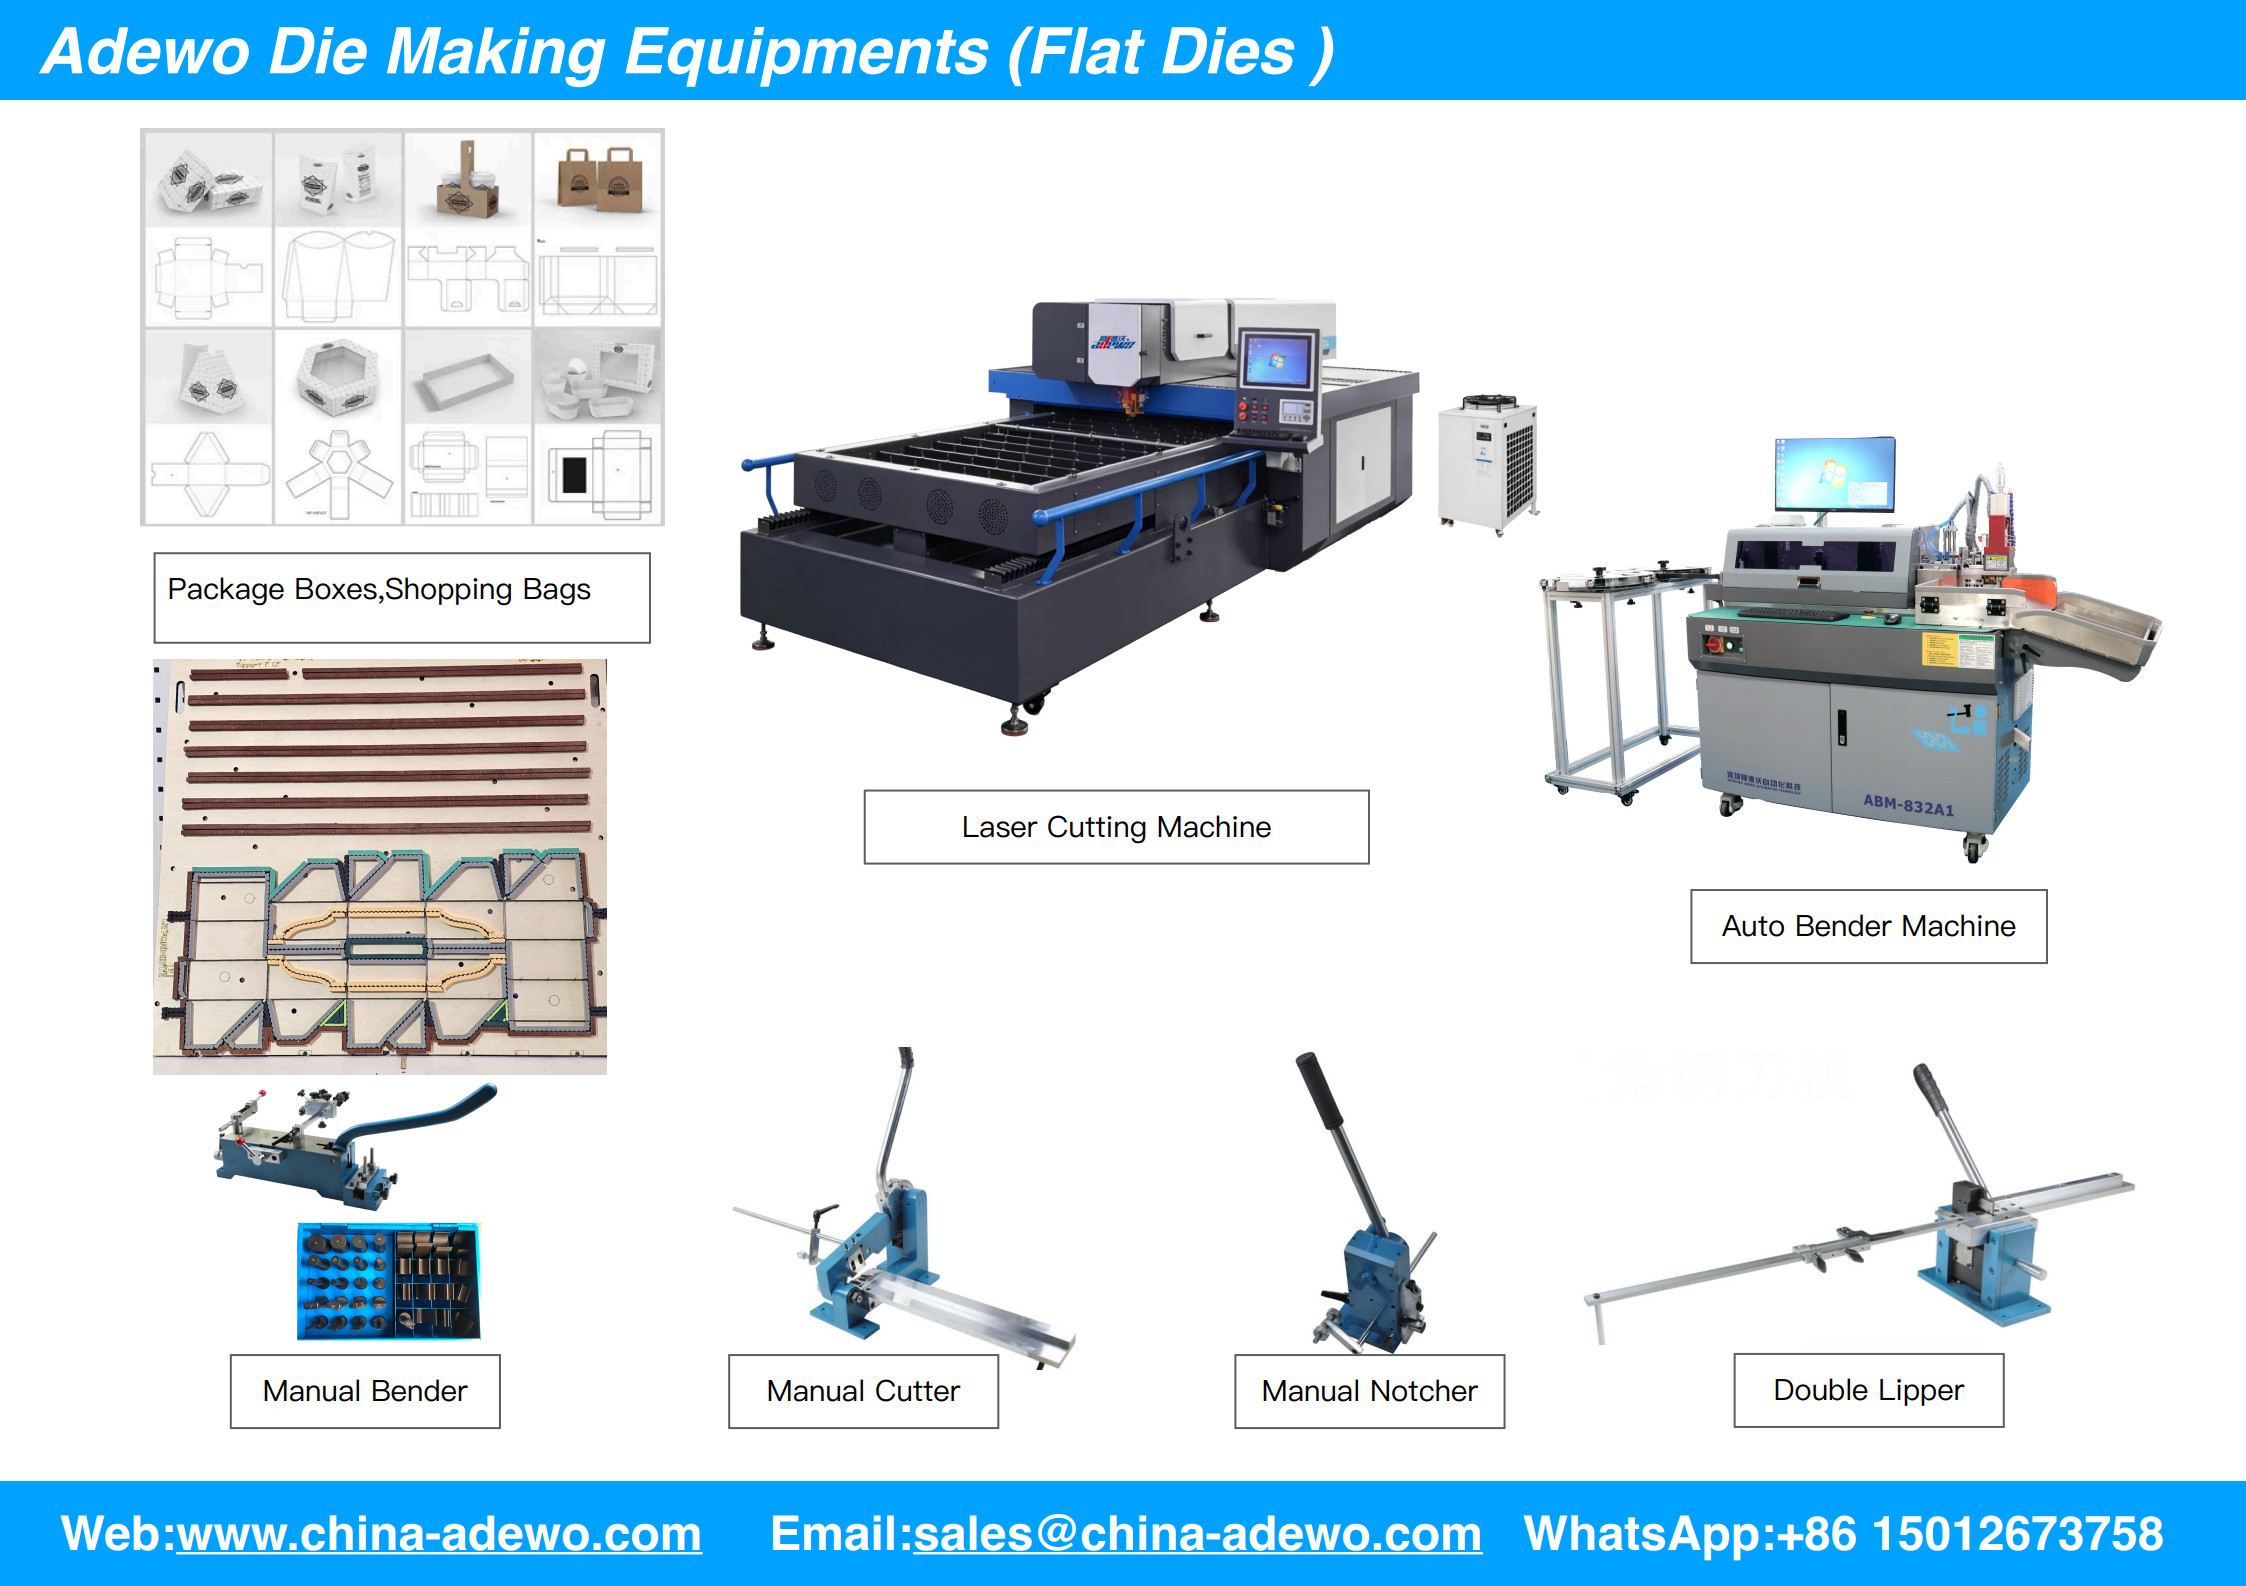
For shops producing complex multi-up layouts or short lead times, yes. Lasers eliminate saw kerf variability, let you cut intricate slots and perforation lines directly from CAD files, and reduce hand-finishing. The payback comes from fewer rejected dies and faster turnaround, not just labor savings.
Daily checks on rule bending heads, laser optics or saw blades, and pneumatic clamps matter more than annual overhauls. Keep cutting beds free of paper dust and adhesive residue, and calibrate the axis every 40–50 operating hours to catch drift before it affects die accuracy.
It's critical when you're working with customer-supplied structural files. Direct import of formats like CFF2 or DXF removes manual redraw errors. Good integration also lets you apply automatic bridges, nicks, and crease offset rules specific to a converter's folder-gluer, which keeps the die compatible downstream.
Look for programmable pin density and individually replaceable ejector strips. Inadequate ejection shows up as jammed blanks or slow stripping on the press. Professional equipment lets you map ejection pressure zones to match blank complexity, reducing wear on both the die and the cutting surface.
Yes, if the equipment supports variable crease rule heights and has multi-axis rule processing. Auto-bottom cartons need folded crease sequences and angled cuts that basic linear systems can't produce cleanly. Modular setups with rotating benders or laser cutting heads are the practical route.
Conclusion
In folding carton production, the steel choice for cutting dies often gets pulled from a tooling catalog rather than the actual board being converted. That shortcut leads to brittle edges or premature wear, because board caliper, recycled content, and coating all change how a rule behaves at the knife. The same logic applies to creasing depth. A channel that is a few thousandths too shallow leaves cartons fighting the folder-gluer, while one too deep cracks the printed surface right at the score. Getting these two details right from the start prevents most finishing-room slowdowns. Stripping pins rarely show up in equipment discussions, but their placement and spring pressure determine whether makeready takes 20 minutes or half a shift. When pins are worn or uneven, sheets hang up, tear, and force operators into constant adjustments that sap throughput.
High-speed presses make any alignment error obvious within the first thousand sheets, long before a full run is wasted. If the die is not square to the cylinder or the chase has shifted during transport, nicked rules and patchy cutting show up immediately. A daily honing habit on cutting rules costs a few minutes but keeps the blade geometry crisp, reducing dust and improving stripping consistency. However, none of this matters if buyers evaluate tooling on the upfront quote alone. The hidden figure is the true cost per million finished cartons, which folds in downtime, rework, scrap, and operator intervention. Equipment that holds registration, keeps crease depth stable, and reduces pin-related stops will pay for itself even if the initial die price is higher. Packaging success is not about buying the cheapest die; it’s about making the entire converting line predictable.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com